

Due to the different production processes of copper rods, the oxygen content and appearance of the copper rods produced are different. The copper rod produced by Shangyin has an oxygen content of less than 10ppm when the process is appropriate, which is called oxygen free copper rod; The copper rod produced by continuous casting is hot-rolled under protective conditions, with an oxygen content ranging from 200-500ppm, but sometimes as high as 700ppm or more. Generally, the copper produced by this method has a bright appearance, and the low oxygen copper rod is sometimes called a polished rod.
Oxygen free copper rod
Copper rod is the main raw material in the cable industry, and there are two main production methods - continuous casting and rolling method and upward continuous casting method. There are many production methods for low oxygen copper bars in continuous casting and rolling. Its characteristic is that after the metal melts in the vertical furnace, the copper liquid enters the closed mold cavity from the pouring pipe through the insulation furnace, chute, and intermediate package, and is cooled with a high cooling intensity to form a cast billet. Then, multiple passes of rolling are carried out to produce low oxygen copper bars with hot working structure. The original casting structure has been broken, and the oxygen content is generally between 200 and 400 ppm. Most of the oxygen free copper rods in China are produced using the upward casting method. The metal melts in an induction furnace and is continuously cast by upward casting through a graphite mold, followed by cold rolling or cold processing. The produced oxygen free copper rods have a casting structure with an oxygen content generally below 20ppm. Due to different manufacturing processes, there are significant differences in organizational structure, oxygen content distribution, impurity form and distribution, and many other aspects.
1, Drawing performance
The drawing performance of copper rods is related to many factors, such as impurity content, oxygen content and distribution, process control, etc. Below, the drawing performance of copper rods will be analyzed from the above aspects.
1. The influence of melting method on impurities such as S
The production of copper rods by continuous casting and rolling mainly involves the combustion of gas to melt the copper rods. During the combustion process, oxidation and volatilization can reduce the entry of some impurities into the copper liquid to a certain extent. Therefore, the requirements for raw materials in continuous casting and rolling are relatively low. During the production of oxygen free copper rods by continuous casting, due to the melting process using an induction furnace, the "copper green" and "copper beans" on the surface of the electrolytic copper are mostly melted into the copper liquid. The melted S has a significant impact on the plasticity of oxygen free copper rods and increases the wire drawing breakage rate.
2. The entry of impurities during the casting process
In the production process, the continuous casting and rolling process requires the transfer of copper liquid through insulation furnaces, chutes, and intermediate packages, which is relatively easy to cause the peeling of refractory materials. During the rolling process, it is necessary to use rollers to cause the detachment of iron, which will cause external inclusions in the copper rod. The rolling of oxides on and under the skin during hot rolling will have adverse effects on the drawing of low oxygen rods. The production process of upward casting method is relatively short, and the copper liquid is completed through the subsurface flow in the joint furnace, which has little impact on the refractory material. Crystallization is carried out through the graphite mold, so there are fewer possible sources of pollution and fewer opportunities for impurities to enter during the process.
O. S and P are elements that produce compounds with copper. In molten copper, oxygen can partially dissolve, but when copper condenses, oxygen is almost insoluble in the copper. The oxygen dissolved in the molten state precipitates as copper oxide eutectic and is distributed at the grain boundaries. The appearance of copper cuprous oxide eutectic significantly reduces the plasticity of copper.
Sulfur can dissolve in molten copper, but its solubility decreases almost to zero at room temperature. It appears in the form of cuprous sulfide at grain boundaries, significantly reducing the plasticity of copper.
3. The distribution and influence of oxygen in low oxygen copper rods and oxygen free copper rods
The oxygen content has a significant impact on the tensile performance of low oxygen copper rods. When the oxygen content increases to the optimal value, the breakage rate of the copper rod is the lowest. This is because oxygen acts as a scavenger in the process of reacting with most impurities. Moderate oxygen is also beneficial for removing hydrogen from copper liquid, generating water vapor overflow, and reducing the formation of pores. The optimal oxygen content provides the best conditions for the wire drawing process.
Distribution of low oxygen copper rod oxide: In the initial stage of solidification in continuous casting, heat dissipation rate and uniform cooling are the main factors determining the distribution of copper rod oxide. Uneven cooling can cause fundamental differences in the internal structure of copper rods, but subsequent thermal processing often damages the columnar crystals, resulting in the refinement and uniform distribution of cuprous oxide particles. The typical situation caused by the aggregation of oxide particles is central explosion. In addition to the influence of oxide particle distribution, copper rods with smaller oxide particles exhibit better tensile properties, while larger Cu2O particles are prone to stress concentration points and fracture.
The oxygen content of oxygen free copper exceeds the standard, causing the copper rod to become brittle, the elongation rate to decrease, the stretching pattern port to appear dark red, and the crystalline structure to become loose. When the oxygen content exceeds 8ppm, the process performance deteriorates, manifested by a significant increase in rod breakage and wire breakage rate during casting and stretching processes. This is because oxygen can form a brittle phase of cuprous oxide with copper, forming a copper cuprous oxide eutectic and distributed in a network structure at the boundary. This brittle phase has high hardness and will detach from the copper body during cold deformation, resulting in a decrease in the mechanical properties of the copper rod, which is prone to fracture during subsequent processing. High oxygen content can also lead to a decrease in the conductivity of oxygen free copper rods. Therefore, it is necessary to strictly control the upward casting process and product quality.
4. The impact of hydrogen
In upward casting, the control of oxygen content is relatively low, and the side effects of oxides are reduced, but the influence of hydrogen becomes a more significant problem. After inhalation, there is an equilibrium reaction in the melt: H2O (g)=[O]+2 [H];
Gas and porosity are formed by the precipitation and aggregation of hydrogen from supersaturated solutions during the crystallization process. The hydrogen precipitated before crystallization can also reduce cuprous oxide and generate water bubbles. Due to the characteristic of upward casting, the copper liquid crystallizes from top to bottom, forming a liquid shape that is approximately conical. The gas released before the crystallization of copper liquid is trapped in the solidified structure during the upward floating process, and pores are formed inside the casting rod during crystallization. When the gas content is low, hydrogen precipitates at the grain boundaries, forming looseness; When the gas content is high, it aggregates into pores, so pores and porosity are formed by both hydrogen and water vapor.
Hydrogen comes from various process links in the production process, such as the raw material electrolytic copper "copper green", auxiliary material charcoal * *, climate environment * *, and graphite crystallizer not yet dried. Therefore, the surface of the copper liquid in the melting furnace should be covered with baked charcoal, and electrolytic copper should try to remove "copper green", "copper beans" and "ears" as much as possible, which is very important for improving the quality of oxygen free copper rods.
In the continuous casting and rolling process, moderate control of oxygen content is often used to control hydrogen. Cu2O+ H2= 2Cu+ H2O
Due to the bottom-up crystallization of molten copper during the casting process, the water vapor generated by oxygen and hydrogen in the molten copper can easily float out, and most of the hydrogen in the molten copper can be effectively removed,Therefore, the impact on the copper rod is relatively small.
2, Surface quality
In the process of producing electromagnetic wires and other products, requirements also need to be placed on the surface quality of copper rods. The surface of the drawn copper wire needs to be free of burrs, less copper powder, and no oil stains. And the quality of the surface copper powder is measured by torsion test, and the recovery of the copper rod after torsion is observed to determine its quality.
During the continuous casting and rolling process, from casting to rolling, the temperature is high and completely exposed to air, causing a thick oxide layer to form on the surface of the cast billet. During the rolling process, as the rolling mill rotates, the oxide particles roll into the surface of the copper wire. Due to the high melting point brittleness of cuprous oxide, when it is rolled deeper into the mold as a strip-shaped aggregate, burrs will form on the outer surface of the copper rod when it is stretched by the mold, causing trouble for subsequent painting.
The oxygen free copper rod manufactured by the upward casting process is completely isolated from oxygen during casting and cooling, and there is no subsequent hot rolling process. The surface of the copper rod has no oxide rolled into the surface, and the quality is good. After drawing, there is less copper powder, and the above problems are less common.
Oxygen free copper rods are also made with imported equipment and domestically produced equipment, but currently imported products have no obvious advantages. The difference between copper rod products is not very significant. As long as the copper plate is well selected and the production control is relatively stable, domestically produced equipment can also produce copper rods that can be stretched by 0.05. Imported equipment is generally from Ottokunp, Finland, and the best domestically produced equipment should be from the Shanghai Navy Factory, with the longest production time and reliable quality for military enterprises.
There are two main types of imported equipment for low oxygen copper rods internationally. One is Southwire equipment from the United States, with domestic manufacturers being Nanjing Huaxin and Jiangxi Copper Industry. The other is CONTIROD equipment from Germany, with domestic manufacturers being Changzhou Jinyuan and Tianjin DaSeamless.
Oxygen free and low oxygen rods are easily distinguished in terms of oxygen content. Oxygen free copper has an oxygen content of 10-20 PPM or less, but currently some manufacturers can only achieve 50 PPM or less. Low oxygen copper rods have an oxygen content of 200-400 PPM, while good rods generally have an oxygen content controlled at around 250 PPM. Oxygen free rods generally use the upward drawing method, while low oxygen rods are continuous casting and rolling. Compared to the two products, low oxygen rods are more suitable for enameled wire performance, such as softness, rebound angle, and winding performance. However, low oxygen rods are relatively more demanding on drawing conditions. Similarly, when drawing 0.2 fine wires, if the drawing conditions are not good, ordinary oxygen rods can be pulled while good low oxygen rods will break. But if placed under good drawing conditions, low oxygen rods will break. The same pole, a low oxygen pole may be able to pull up to 0.05, while a regular anaerobic pole can only stretch up to 0.1 at most, Of course, the finest ones like Double Zero must rely on imported oxygen free copper rods. Currently, some companies are trying to use skinning to treat low oxygen rods to stretch 0.03 lines. However, I am not very clear about this aspect.
Low oxygen copper rod
Audio cables generally prefer to use oxygen free rods, which is related to the fact that oxygen free rods are made of monocrystalline copper and oxygen free rods are made of polycrystalline copper.
Low oxygen copper rods and oxygen free copper rods have their own characteristics due to differences in manufacturing methods.
1, Regarding the inhalation and removal of oxygen and its existence status
The oxygen content of cathode copper for producing copper rods is generally between 10-50ppm, and the solid solubility of oxygen in copper at room temperature is about 2ppm. The oxygen content of low oxygen copper rods is generally between 200 (175) and 400 (450) ppm, so oxygen is inhaled in the liquid state of copper. On the other hand, oxygen in oxygen free copper rods with upward drawing method is the opposite. After being held in liquid copper for a considerable period of time, oxygen is reduced and removed. Usually, the oxygen content of such rods is below 10-50 ppm, and the lowest can reach 1-2 ppm. From a tissue perspective, oxygen in low oxygen copper exists in the form of copper oxide near the grain boundary, which is common for low oxygen copper rods but rare for oxygen free copper rods. The appearance of copper oxide in the form of inclusions at grain boundaries has a negative impact on the toughness of the material. And oxygen in oxygen free copper is very low, so the structure of this copper is a uniform single-phase structure, which is beneficial for toughness. Porosity is uncommon in oxygen free copper rods, while it is a common defect in low oxygen copper rods.
2, The difference between hot-rolled structure and cast structure
Due to hot rolling, the microstructure of low oxygen copper rod belongs to the hot working microstructure, and the original cast microstructure has been broken. It has already appeared in the form of recrystallization at the 8mm rod, while oxygen free copper rod belongs to the cast microstructure with coarse grains. This is the inherent reason why the recrystallization temperature of oxygen free copper is higher and requires a higher annealing temperature. This is because recrystallization occurs near the grain boundaries, and the oxygen free copper rod has coarse grains with grain sizes up to several millimeters, resulting in fewer grain boundaries. Even through drawing deformation, the grain boundaries are relatively fewer compared to oxygen free copper rods, requiring higher annealing power. The requirement for successful annealing of oxygen free copper is that the first annealing of a wire drawn from a rod but not yet cast should have an annealing power 10-15% higher than that of low oxygen copper under the same conditions. After further drawing, sufficient margin should be left for annealing power in the later stages, and different annealing processes should be performed to distinguish between low oxygen copper and oxygen free copper, in order to ensure the flexibility of the wire in process and finished products.
3, Differences in inclusions, fluctuations in oxygen content, surface oxides, and possible hot-rolled defects
The pull-out performance of oxygen free copper rods is superior to that of low oxygen copper rods in all wire diameters. In addition to the aforementioned structural reasons, oxygen free copper rods have fewer inclusions, stable oxygen content, and no defects that may occur during hot rolling. The oxide thickness on the rod surface can reach ≤ 15A. If the process is unstable and oxygen monitoring is not strict during continuous casting and rolling production, the unstable oxygen content will directly affect the performance of the rod. If the surface oxide of the rod can be compensated for in the continuous cleaning of the subsequent process, but the more troublesome thing is that there is a considerable amount of oxide present in the "subcutaneous" area, which has a more direct impact on wire breakage. Therefore, when drawing micro fine wires and ultrafine fine wires, in order to reduce breakage, sometimes the copper rod must be subjected to a last resort - peeling, or even secondary peeling. The reason for this is to remove subcutaneous oxide.
4, There is a difference in toughness between low oxygen copper rods and oxygen free copper rods
Both can be pulled up to 0.015mm, but in low-temperature grade oxygen free copper in low-temperature superconducting wires, the spacing between the filaments is only 0.001mm
5, There are differences in the economic efficiency from the raw materials used to make the rods to the production lines.
Manufacturing oxygen free copper rods requires high-quality raw materials. Generally, when drawing copper wires with a diameter greater than 1mm, the advantages of low oxygen copper rods are more obvious, while oxygen free copper rods are more advantageous when drawing copper wires with a diameter less than 0.5mm.
6, The production process of low oxygen copper rods is different from that of oxygen free copper rods.
The production process of low oxygen copper rods cannot be transferred to the production process of oxygen free copper rods, at least the annealing processes of the two are different. Because the flexibility of the wire is deeply influenced by the material composition, rod making, wire making, and annealing processes, it cannot be simply said that low oxygen copper or oxygen free copper is softer and harder.
Introduction to Low Oxygen Copper Rod and Oxygen Free Copper Rod
1. Low oxygen copper rod
What is a low oxygen copper rod? What is the production process of low oxygen copper rod? What are the introductions to low oxygen copper rods? Firstly, let's take a look at the definition of low oxygen copper rods: copper rods with an oxygen content between 200 (175) and 400 (450) ppm are produced through continuous casting and rolling methods using copper as raw material.
Introduction to Low Oxygen Copper Rod - Process Flow of Low Oxygen Copper Rod:
Low oxygen copper rods are produced using continuous casting and rolling technology. The process flow is as follows: electrolytic copper → vertical furnace → insulation furnace → casting machine → continuous rolling machine → cleaning → rod closing machine → finished product (ф 8mm) electrolytic copper is continuously fed, melted continuously in the vertical furnace, and copper water is released. The large cross-section trapezoidal ingot is cast by the casting machine and enters the rolling mill for hot rolling, resulting in a ф 8mm copper rod billet.
▍ Process defects
(1) Vertical furnace: A. Due to its small volume, electrolytic copper is melted while being added, and there is no condition for the molten copper water to be fully reduced B. The entire melting process and copper production process cannot be separated by oxygen, so the oxygen content is very high C. Molten copper fuel is generally a gas, and during the combustion process of the gas, it directly affects the chemical composition and properties of the copper liquid, with significant impacts such as sulfur and hydrogen.
(2) Casting machine: During the process of the crystallization wheel of the casting machine turning the copper liquid into a solid, oxygen isolation cannot be carried out, so a second large amount of oxygen absorption is carried out during the casting process.
(3) Temperature control: A. Copper liquid temperature, due to the large rolling volume and various factors, this temperature is not easy to control. B. The temperature of the ingot entering the rolling mill is required to be controlled at 850 ℃. The larger the deviation between the upper and lower parts, the greater the impact on the quality of the copper rod, and this temperature is difficult to control. C. The temperature of the copper rod in the rolling mill is required to be controlled at 600 ℃, and the larger the deviation between the upper and lower parts, the greater the impact on the quality of the copper rod. Due to the constraints of the previous process, it is also difficult to control this temperature. D. There are many links in the entire process, and any slight problem in one link can affect temperature control.
(4) Other: A. Due to the above-mentioned defects, the quality of the copper rod may be unstable. Therefore, the standard stipulates that before leaving the factory, low oxygen copper rods produced by continuous casting and rolling must undergo a torsion test. But some production plants do not do it at all, or do not produce in batches according to regulations (each batch should not exceed 60 tons), or reverse the unqualified batches and still leave the factory. B. High oxygen content will affect the wire drawing process, and the copper wire will become harder as it is pulled, requiring additional annealing in the middle. High oxygen content can also affect conductivity. C. To solve the process defects, it is necessary to improve the performance of the unit as much as possible, so the unit price is expensive. For example, the annual production of 24000 to 40000 tons of units by the American Southern Company is priced at 6.9 million US dollars, while the German Krupp Company is even more expensive. And the user's own supporting facilities also cost hundreds of thousands or even millions of dollars.
Process advantages: (1) High output, generally small units can produce 10-14 tons per hour. (2) The copper rod unloading adopts a plum blossom style, which is convenient for the wire drawing machine to release the wire. (3) The weight of the wire is large, usually up to 4 tons per plate.
Introduction to Low Oxygen Copper Rod - Copper Rod Production Process Method:
1. Dip coating molding method: capable of producing long length bright oxygen free copper rods with conductivity of 101-102% IACS, oxygen content below 20ppm, and copper rod coil weight of 3.5-10 tons.
Dip coating molding utilizes the heat absorption ability of a cold copper rod. A relatively thin, cold pure copper core rod (also known as a seed rod) is vertically passed through a copper water tank that can maintain a certain liquid level. The copper water is fused with the copper on the surface of the moving seed rod, and gradually solidifies and combines into a coarser cast copper rod. Then, it is cooled, hot-rolled, cooled, and wound into a circle. The entire process is enclosed and protected by inert gas.
2. Upward cold rolling method: capable of producing long length bright oxygen free copper rods with conductivity of 101-101.6% IACS, oxygen content below 10ppm, and copper rod coil weight of 2 tons.
It uses a tubular copper sleeve (i.e. graphite crystallizer) with its lower end immersed in the molten copper liquid surface and its upper end connected to a vacuum pump. At the beginning, the air inside the crystallizer is extracted, and under the action of vacuum, negative pressure is generated inside the tube. The copper liquid is slowly attracted upwards and quickly solidifies into a bright ingot near the elevator. Then it is cold-rolled or cold drawn into a rod. The copper rod produced by the upward method has an oxygen content of less than 10ppm and a bright surface.
3. Continuous casting and rolling method: capable of producing long length bright low oxygen copper rods with conductivity of 101-102% IACS, oxygen content of 200-300ppm, and copper rod coils weighing up to 5 tons.
4. Loop rolling method: Produce short length oxidized black copper rods with conductivity of 99.5-100.5% IACS, oxygen content of 200-500ppm, and copper rod coil weight of only 86-136 kilograms. (Due to weight limitations of ship shaped copper ingots)
Introduction to Low Oxygen Copper Rod - Low Oxygen Copper Rod Grades and Characteristics:
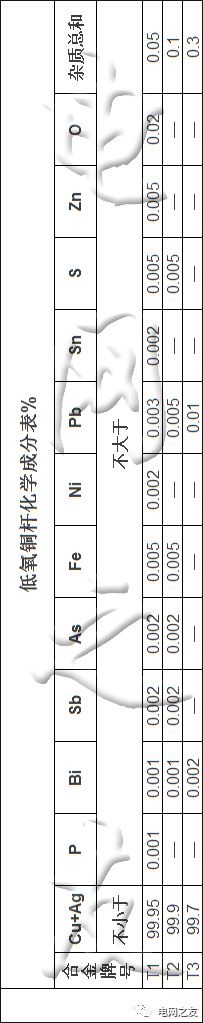
There are three grades of low oxygen copper rods, T1, T2, and T3. Low oxygen copper rods are all hot-rolled, so they are called soft rods with the code R.
(1) T1: Produce low oxygen copper rods using high-purity electrolytic copper as raw material (with a copper content greater than 99.9975%).
(2) T2: Using 1 # electrolytic copper as raw material (with a copper content greater than 99.95%) to produce low oxygen copper rods.
(3) T3: Use 2 # electrolytic copper as raw material (with a copper content greater than 99.90%) to produce low oxygen copper rods. Due to the scarcity of high-purity electrolytic copper and 2 # electrolytic copper in the market, 1 # electrolytic copper is generally used as the raw material, so the general low oxygen copper rod grade is T2R.
Introduction to Low Oxygen Copper Rod - Chemical Composition Table of Low Oxygen Copper Rod:
2. Oxygen free copper rod
Due to different production processes of copper rods, the oxygen content and appearance of the copper rods produced are different. The copper rod produced by Shangyin has an oxygen content below 20ppm when the process is appropriate, which is called oxygen free copper rod; The copper bars produced by continuous casting and rolling are hot-rolled under protective conditions, with oxygen content ranging from 200-500ppm, but sometimes as high as 700ppm or more. Generally, the copper produced by this method has a bright appearance, commonly known as bright bars.
Oxygen free copper rod is pure copper that does not contain oxygen or any residual deoxidizer. But in reality, it still contains very trace amounts of oxygen and some impurities. According to the standard regulations, the oxygen content should not exceed 0.02%, the total impurity content should not exceed 0.05%, and the purity of copper should be greater than 99.95%.
Generally, electrolytic copper is used for production, and its resistivity is lower than that of low oxygen copper rods. Therefore, in the production of products with strict resistance requirements, oxygen free copper rods are more economical; Manufacturing oxygen free copper rods requires high-quality raw materials; The oxygen free copper rod is more superior in drawing copper wires with a diameter of less than 0.5mm. 6MM oxygen free copper rod is used for producing copper flat wire. 3mm oxygen free copper rod is used for wire drawing, production of wire copper core, and enameled wire. Mainly used for wires, cables, and motors.
According to the oxygen content and impurity content, oxygen free copper rods are divided into TU1 and TU2 copper rods. The purity of TU1 oxygen free copper rod reaches 99.99%, and the oxygen content is not greater than 0.001%; The purity of TU2 oxygen free copper reaches 99.95%, and the oxygen content is not greater than 0.002%.


